Les grades de PA6 chargés de minéraux utilisent un renfort minéral pour ajuster la rigidité et le comportement dimensionnel ; leur sélection nécessite toutefois des données spécifiques à chaque grade et des essais sur les pièces.
PA6 mineral-filled nylon, often called PA6-MD, is selected when a molded part needs better dimensional stability and lower warpage than unfilled PA6 without the full stiffness or fiber-orientation effect of a glass- or carbon-filled grade. The filler does not remove nylon’s moisture sensitivity, so material selection, drying, mold temperature, wall design and inspection condition must be reviewed together.

What Is PA6 Mineral-Filled Nylon?
PA6-MD is a nylon 6 compound containing mineral additives such as talc, calcium carbonate or wollastonite. The filler reduces the resin fraction that drives shrinkage and can improve surface hardness and dimensional consistency. The tradeoff is lower tensile strength than a comparable glass-filled grade and a different balance of impact, weld-line and processing behavior.
Mineral-filled PA6 is a material family, not one universal grade. Filler loading, particle treatment, color package, stabilizers and processing history can change the result. Ask for the exact grade and lot documentation instead of approving a part from the words “mineral filled” alone.
| Material route | Main advantage | Main watch-out | Typical decision |
|---|---|---|---|
| PA6 non chargé | Balanced toughness and flow | Moisture response and higher molding shrinkage | General molded parts where flexibility matters |
| PA6-MD | Lower warpage and better surface stability | Lower strength than a reinforced grade | Flat housings, covers and dimensional parts |
| PA-GF20 | Higher stiffness and load capability | Fiber orientation, anisotropic shrinkage and surface fiber | Structural parts with a defined load path |
| PA-CF30 | High stiffness and low expansion in selected directions | Cost, processing wear and strong orientation effects | Stiff, dimension-critical parts after validation |
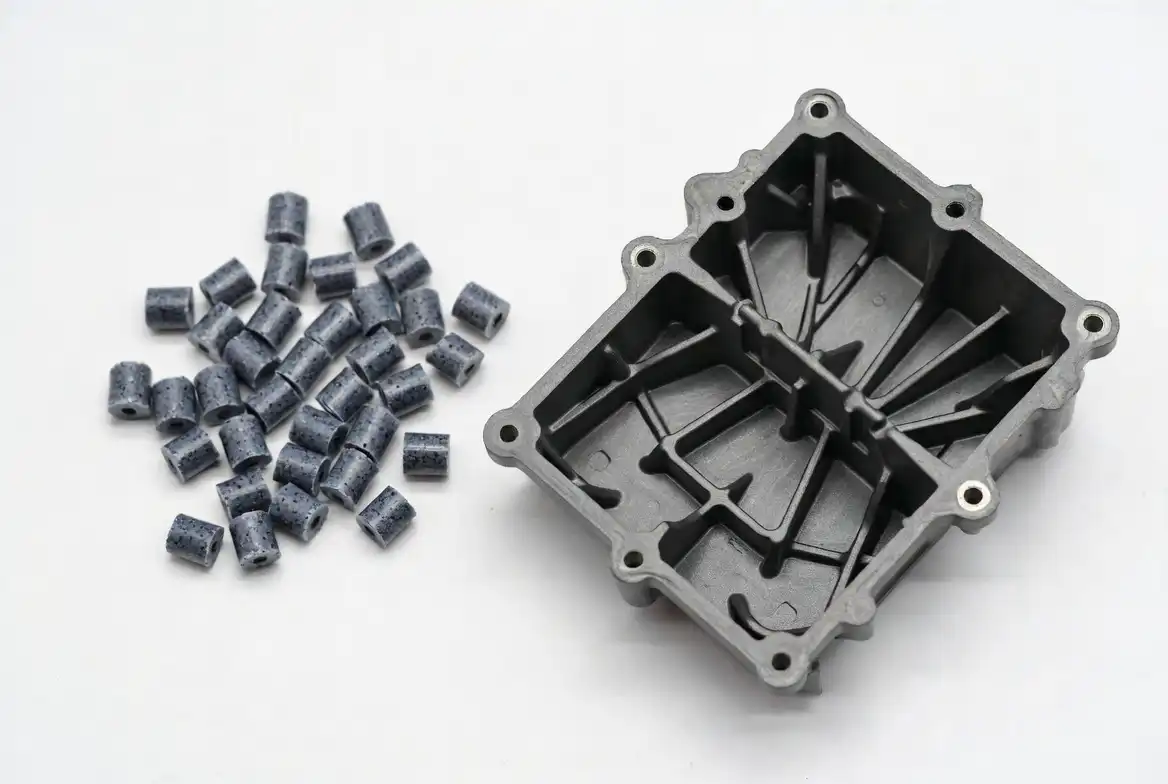
Designing Parts for Low Warpage
PA6-MD can reduce warpage risk, but it cannot correct a poor geometry. Keep wall thickness as uniform as the function allows, avoid abrupt mass changes, support flat panels with ribs and place ribs so they do not create an uncontrolled sink or cooling difference. Gate location, flow length and cooling-channel layout still influence the final shape.
Define the measurement condition before the tool is released. Nylon dimensions change with moisture and temperature, so a supplier needs the conditioned state, critical datum scheme, tolerance stack and functional fit requirement. Measuring a dry part in a warm inspection room and comparing it with a conditioned drawing can create a false process problem.
Processing and Drying Controls
PA6-MD must be dried according to the compound supplier’s data sheet. A common starting point is a desiccant dryer near 80 C for several hours, with a verified moisture target often below 0.15 percent, but the exact value depends on the grade, packaging and residence time. Keep the material sealed after drying and record dryer temperature, time and moisture checks.
Mold temperature, fill profile, packing, gate seal and cooling time should be validated on the actual cavity. Mineral filler may improve dimensional stability, but it can also change flow resistance and weld-line behavior. Do not copy a PA-GF20 or unfilled PA6 setup sheet without a short-shot review and dimensional study.
Inspection and Production Validation
- Approve the exact resin grade, filler level, color and moisture condition.
- Measure critical dimensions at the agreed temperature and conditioning state.
- Compare flatness, hole position, boss location and mating fit across multiple cavities and lots.
- Record process window limits rather than approving one favorable sample.
- Revalidate when the grade, mold revision, gate, drying process or inspection method changes.
How Nylon Plastic Supports Material Selection
Nylon Plastic supports material modification and molded plastic-part development from resin selection through DFM, sampling and production review. For a PA6-MD decision, the useful comparison includes unfilled PA, PA-GF20 and PA-CF30 when the application needs a different balance of strength, stiffness, warpage, wear or cost. The objective is a grade that can be purchased consistently and validated in the finished part.
Lire la suite
- Guide du moulage par injection
- Services de moulage par injection de nylon
- Guide des matières plastiques
Questions fréquemment posées
Que signifie « MD » dans « PA6-MD » ?
MD signifie « chargé en minéraux ». Des additifs minéraux tels que le talc, le carbonate de calcium ou la wollastonite sont incorporés au PA6 afin de réduire le retrait et d'améliorer la stabilité dimensionnelle.
En quoi le PA6 chargé de minéraux se distingue-t-il du PA-GF20 ?
Le PA6-MD privilégie généralement un gauchissement réduit et une surface plus stable, tandis que le PA-GF20 offre généralement une rigidité et une capacité de charge supérieures. Le choix approprié dépend des contraintes en matière de résistance, de planéité, de résistance aux chocs et d'orientation des fibres.
Quelles sont les teneurs habituelles en charges minérales dans le PA6-MD ?
Les nuances commerciales varient, et de nombreuses nuances techniques se situent globalement dans une fourchette de 20 à 40 %. Vérifiez le type exact de charge et sa teneur dans la fiche technique de la nuance, car la teneur en charge influe sur la fluidité, la résistance et le retrait.
Le PA6 chargé de minéraux doit-il être séché avant le moulage ?
Yes. The mineral filler does not eliminate nylon moisture sensitivity. Dry the compound to the supplier’s target, keep it sealed and verify moisture before molding.
Le PA6-MD permet-il d'éliminer complètement le gauchissement ?
Non. Cela peut réduire les mouvements liés au retrait, mais l'emplacement de l'entrée de coulée, l'épaisseur de paroi, l'équilibre de refroidissement, le compactage, l'humidité et les conditions de mesure restent déterminants pour la forme finale.
Que doit contenir un appel d'offres pour du PA6-MD ?
Include the part CAD and drawing, flatness and dimensional limits, service temperature, moisture or chemical exposure, annual volume, exact material preference and the required inspection condition.
Request a PA6-MD Material Review
Send the part drawing, flatness and tolerance requirements, service environment, annual volume and preferred PA6-MD or reinforced nylon grade.

