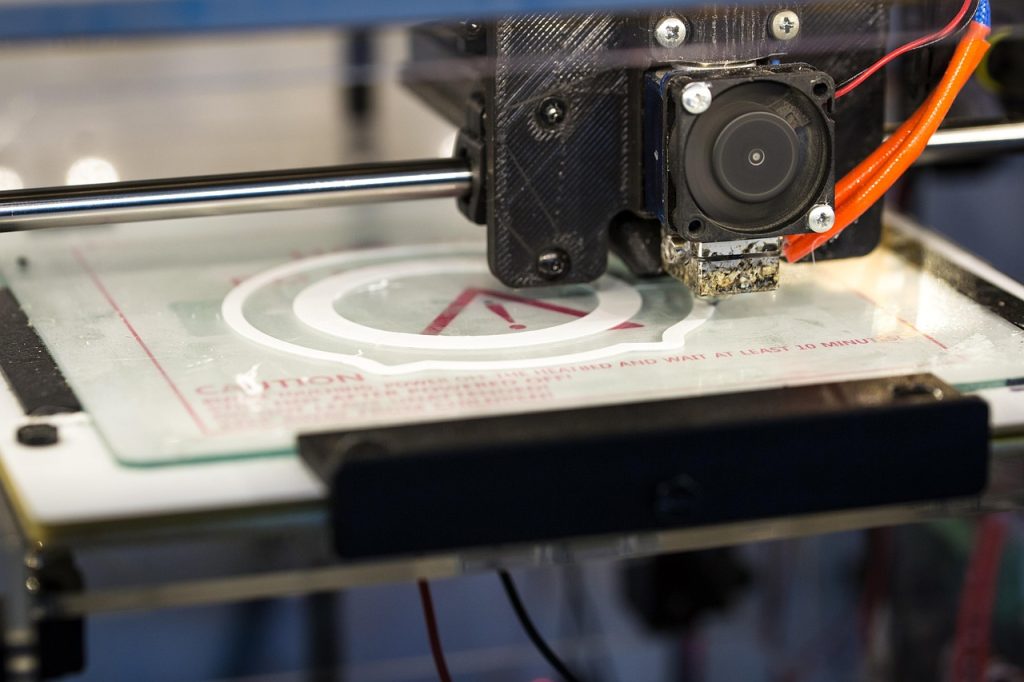
Le post-traitement du PETG comprend le ponçage, le polissage, le revêtement et le collage, tout en préservant la précision dimensionnelle et les performances des assemblages.
Les impressions en PETG peuvent être poncées, revêtues et collées, mais la chaleur et les solvants peuvent altérer la surface ou déformer une pièce ajustée avec précision. Commencez par définir l'aspect souhaité et la résistance requise des joints, puis testez la méthode de finition sur une impression de test. Ce guide aborde les étapes de ponçage et de polissage, le revêtement, le collage ainsi que les problèmes courants liés à la finition.

Pourquoi procéder à un post-traitement du PETG ?
Les impressions en PETG brut présentent des lignes de couche visibles et peuvent ne pas répondre aux exigences esthétiques ou fonctionnelles des produits finis. Le post-traitement permet :
- Améliorer la finesse de la surface pour un rendu esthétique
- Prepare surfaces for an agreed coating or assembly method
- Improve appearance while leaving sealing performance to a separate test
- Activer la peinture et la finition
If you’re still deciding between materials, les fonctionnalités de post-traitement pourraient influencer votre choix.
Ponçage du PETG

Point de départ
Start on a spare print. Use the least aggressive abrasive that removes the visible layer steps without rounding the features you need to keep. Work through finer abrasives only after the previous scratches are removed; a particular grit sequence does not guarantee clarity.
La technique, ça compte
Use light pressure and check for heat, smearing and edge rounding. Wet sanding can help control dust and clogging where suitable for the part. Keep water away from powered equipment and let the part dry before applying an adhesive or coating.
Prusa’s PETG guide confirms both dry and wet sanding. Mask locating faces and sealing surfaces that must retain their dimensions.
Exemple de progression
| Stade | Work to an observed result | Check before continuing |
|---|---|---|
| Remove layer peaks | Stop when the ridges are reduced without losing the intended shape | Wall thickness, edges, holes and snap features |
| Refine scratches | Use successively finer abrasives on the same sample | Even scratch pattern; no local heat smearing |
| Polish or coat | Trial the selected finishing system on the spare print | Appearance, added thickness, adhesion and full cure per supplier |
| Accept the part | Inspect after cleaning and finishing | Critical dimensions and any agreed joint or leakage test |
Lissage chimique
Acetone vapor is not a normal PETG finishing route. Prusa describes chemical dissolution using hazardous laboratory chemicals; this guide does not recommend it for a workshop finishing process. Begin with controlled sanding and a compatible coating when appearance is the goal.
Heat and Dimensional Risk
A heat-gun setting is not the temperature of the plastic. Local heat can round an edge, change a hole or warp a thin cover before the whole surface looks finished. Do not treat a fixed gun temperature and distance as a qualified process for a fitted or loaded part.
Coating Trials
Choose a coating whose supplier supports the substrate and exposure. Follow its surface preparation, mixing, ventilation, cure and thickness instructions. Check adhesion and fit on a spare print; neither a glossy surface nor a coating alone establishes watertightness.
Assemblage de pièces en PETG

Choose the joint geometry and service load before choosing an adhesive. Surface preparation, bond-line thickness, cure conditions and moisture exposure can change the outcome.
Cyanoacrylate and Epoxy
Use an adhesive supplier’s PETG or copolyester guidance for the exact product. Fixture time and full cure are different; there is no universal 60-second hold or 24-hour cure for all systems. Check a representative bonded coupon before relying on the assembly.
Welding and Mechanical Joints
Welding can be considered where the material and geometry support it, but a filled seam is not proof of joint strength. Compare a qualified weld, adhesive joint and mechanical fastening where appropriate. Agree the acceptance load and inspect the complete joint after the intended exposure.
For a quotation, include the split line, overlap or fastening geometry, appearance target and surfaces that must remain free of adhesive or coating.
Masticage et peinture
Trial primer, filler and topcoat as a complete compatible system. Follow each supplier’s preparation, flash and cure instructions. A solvent or cleaner that seems harmless on an offcut may still affect a stressed feature; test the actual material before committing to a batch.
Keep coatings off critical bores, sealing faces and locating datums unless the drawing allows their thickness. Specify whether the target is an even satin appearance, gloss or a particular color reference.
Dépannage
Sanding Leaves White Marks or Smearing
Stop and inspect the spare sample. Abrasion scratches, local heating and stress can look similar. Change pressure and abrasive progression one variable at a time before treating the finished part.
The Finish Changes the Fit
Check material removal, coating thickness and distortion against the drawing. Mask critical interfaces or leave a defined finishing allowance on the next build.
A Bond Fails Under Load
Review joint geometry, cleaning, adhesive compatibility and full cure before changing products. Repeat the load and exposure test on a representative joint; switching to epoxy or welding does not by itself qualify it.
Request Finished PETG Parts
Send the CAD or drawing, quantity, finish reference, critical dimensions and joint loads. Mark which faces can be sanded or coated. We can review the printing route and finishing scope together before a representative sample is approved. Discuss the part and finish.
Questions fréquemment posées
Peut-on poncer et polir les impressions en PETG ?
Oui. Utilisez des abrasifs de plus en plus fins et veillez à maintenir une faible température ; le ponçage à l'eau permet de réduire le colmatage et les traces sur la surface. Testez le résultat sur un tirage de réserve avant de traiter une partie visible.
Les vapeurs d'acétone permettent-elles de lisser le PETG ?
Le PETG ne réagit pas aux vapeurs d'acétone comme l'ABS. Pour obtenir un aspect plus lisse, pensez à poncer soigneusement la pièce avant d'appliquer un revêtement compatible, et testez d'abord la finition.
Quelle est la meilleure façon d'assembler deux pièces en PETG ?
Le choix dépend de la charge exercée sur l'assemblage et de la qualité de l'ajustement. Le cyanoacrylate peut convenir aux petits assemblages soumis à de faibles charges ; pour les autres assemblages, on peut envisager une soudure à l'époxy ou au PETG compatible. Préparez et testez l'assemblage réel avant de vous y fier.
La finition peut-elle avoir une incidence sur les dimensions ou la résistance du PETG ?
Oui. Le ponçage enlève de la matière, la chaleur peut déformer les éléments et un revêtement ajoute de l'épaisseur. Définissez les cotes critiques et les charges aux joints avant la finition, puis inspectez la pièce finie.